Diff bearing replacement - shim location (and pinion shaft length?) change in 2014?

Disclaimer: Links on this page pointing to Amazon, eBay and other sites may include affiliate code. If you click them and make a purchase, we may earn a small commission.

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
I'm in the middle of rebuilding (bearings only) my 3.92 rear end on my 2014 1500.

Apparently around 2014 they moved the pinion shims from the shaft (between gear and cone) to the housing (behind cup). It is also MUCH THICKER - mine is 0.067".

The rebuild kit I got does not include that shim - just the shims for the older style - and says it's good for all 4G date range.

You can't just 'change to the other style' and move your shimming, because then you'd have to compress the crush sleeve an extra 0.067" to compensate for the reduced length of the rotating assembly - good effing luck with that.

So just wondering what other people have run into with this. I'm just going to go to the dealer and get a replacement shim (wrecked mine driving out the cup - idk how you could pull it without damaging the shim).

Just looking for some confirmation I'm not insane. Cannot find any mention of this in any videos or in rebuild kits. Except one unanswered old thread on the site where I guy was struggling with this too.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
Oh and spoiler alert - if you drive you're pinion bearing cup out with a chisel or air hammer like all the videos show - on the 2014+ you will be mangling that shim. Pre 2014 you're just hammering on the old cup which doesn't matter. So use a soft drift or something, or just plan to buy a new one.
 

pacofortacos

Senior Member
Joined
Apr 18, 2017
Posts
3,918
Reaction score
5,020
Ram Year
2016
Engine
5.7
Hmm, they show it clear as day in the parts breakdown as being behind the bearing, not the cup.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
Hmm, they show it clear as day in the parts breakdown as being behind the bearing, not the cup.
Yeah that's the crazy part. The only place I found confirmation that mine's not mixed up (other than I bought the truck new in 2014) is the service manual shows it in the right place. In total contradiction of the diagram in the parts manuals, and every youtube video or guide I've found.

I have one on order - and fingers crossed in a week, I can put it back together. And hopefully the new bearings don't throw the depth off much to need reshimming - they shouldn't.

If you were replacing the gears and had to re-shim it, what a headache - idk how you'd do it. Although maybe you could fine tune it with the old style shims you get in the kits... a few thousandths isn't going to matter for the crush sleeve.
test.jpg
 

pacofortacos

Senior Member
Joined
Apr 18, 2017
Posts
3,918
Reaction score
5,020
Ram Year
2016
Engine
5.7
I wonder if it really matters where the shims are, it's just on one side or the other side of the same bearing - though I could see where it could make a difference if they were huge shims but a few thousands on one side vs. the other side of a bearing, I just don't know if it matters.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
I wonder if it really matters where the shims are, it's just on one side or the other side of the same bearing - though I could see where it could make a difference if they were huge shims but a few thousands on one side vs. the other side of a bearing, I just don't know if it matters.
I was thinking that at first, but this shim is very thick - probably 0.050 thicker than those in other spot. So you would have to crush the crush sleeve an extra 0.050. 200ft lbs crushes it about 0.015, so that's like 5x as much work. Watch the videos of guys tightening up that crush sleeve on 5ft breaker bars. The pinion gear would be in the right spot but you the shaft length would be too long and you couldn't crush it enough to pre-load it.

And even if you wanted to try, the shims that come in the kits wouldn't get you the thickness you'd need in the old location if you did want to swap. You'd have to get a bunch of kits or find your own to make up 0.067" range of thickness.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
One bit of good news - the part came in and is the correct replacement shim I need - so the parts diagram in the Mopar system is wrong for these years - I guess they figured it was close enough and you could figure it out.

Now I get to see if I can get it back together right.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
Don't bother trying to use a puller to get the cones off the pinion and 2 carrier bearings. No chance - especially with this no-shim-there-so-no-gap-for-puller config.

Cut the cage and rollers off with a grinding wheel (easy). Then put a deep cut with a grinding wheel in the bare race itself, being careful not to go through to the shaft obviously. Then take a chisel and put it in the groove and give it a whack, and the bearing cracks surprising easily - even easier if you can whack it towards one edge instead of the middle (start the crack from one end) and use a thin cutting wheel and fat chisel so the chisel is spreading the groove, rather than bottoming out. Bearing steel is extremely hard, but also very brittle and cracks easily.

Two trips to Harbor freight, a couple wasted hours... then gave up and just did this and it was maybe 10 minutes each.
IMG_9649.JPG
 

pacofortacos

Senior Member
Joined
Apr 18, 2017
Posts
3,918
Reaction score
5,020
Ram Year
2016
Engine
5.7
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
I saw one video where a guy used that style and I think it worked for him. Now I see that listing it looks like it's very specific and very close fit to the particular bearing probably - so that outer shell holds all the pieces together from blowing apart when you are actually pulling on the outer part of the bearing set, rather than trying to get a knife edge in between the cone and shaft like the generic 'knife edge' ones that I tried.
I'd be interested to see it it in use up close how it manages - but good to know about those. Definitely seems more promising than this style I failed with:

1794233702558.png
 

pacofortacos

Senior Member
Joined
Apr 18, 2017
Posts
3,918
Reaction score
5,020
Ram Year
2016
Engine
5.7
It's not as specific as it might seem, there's a bolt on the side of the outer shell that you tighten against the inner clams.
I thought no way is this going to get the zero clearance side differential bearing off - it did no problem.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
I did look at some videos about those after seeing your post - was curious what they did differently, and you're right - I wasn't understanding how it worked. This youtube video does a really good job of explaining and showing the details of how it works and where it's engaging. It actually is pulling on the cage (which would totally explode if you did it with a simple puller) - but by sandwiching the whole bearing with cone in position within the tool, it makes that work and generally doesn't even damaging the bearing. It's cool - it sandwiches it with a big ring, but it *also* compresses the cup on the cone like it's assembled in the truck. Pretty clever.

Good to know for next time! My 2014 only has about 90k miles on it - but almost 30k is towing a 7000lb trailer around the country, so I guess that's fair to have cooked 2 bearings. Axles and wheel bearings weren't even bad though.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
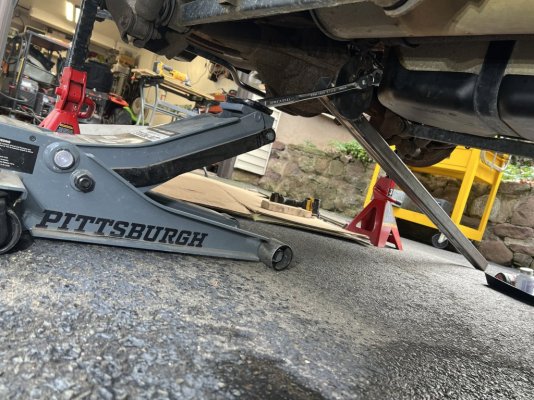
If anyone stumbles across this thread in the future, let it be knowns this is a very involved job. Crikey! Hard with a lift, just utter ***** on your back with jack stands. I'm not going to brag like some youtuber that I did it in X hours. Straight dope - it's taken me a lot of time (plus waiting for parts). I am slow with stuff anyway though, to be fair.

So far I haven't ruined anything but I'd definitely fork over some solid cash to pay someone to do this one next time if i knew they wouldn't screw it up anyway. But good practice if you like tinkering or as a hobby though and aren't in a rush to drive to work in the morning.

I've almost got the pinion nut torqued down properly... but it got dark and didn't want to rush that step - it's the "return to go and start over" step if you over-torque it and I don't think my psyche could take that right now.

And yes I know I'm not a good welder.
 

Attachments

  • IMG_9681.JPG
    IMG_9681.JPG
    121.7 KB · Views: 1
  • IMG_9682.JPG
    IMG_9682.JPG
    142.1 KB · Views: 1
  • IMG_9684.JPG
    IMG_9684.JPG
    227 KB · Views: 1

Hagar1

Senior Member
Joined
Aug 9, 2023
Posts
1,297
Reaction score
2,798
Location
Ontario Canada
Ram Year
2012 Ram 1500
Engine
Hemi 5.7
Don't bother trying to use a puller to get the cones off the pinion and 2 carrier bearings. No chance - especially with this no-shim-there-so-no-gap-for-puller config.

Cut the cage and rollers off with a grinding wheel (easy). Then put a deep cut with a grinding wheel in the bare race itself, being careful not to go through to the shaft obviously. Then take a chisel and put it in the groove and give it a whack, and the bearing cracks surprising easily - even easier if you can whack it towards one edge instead of the middle (start the crack from one end) and use a thin cutting wheel and fat chisel so the chisel is spreading the groove, rather than bottoming out. Bearing steel is extremely hard, but also very brittle and cracks easily.

Two trips to Harbor freight, a couple wasted hours... then gave up and just did this and it was maybe 10 minutes each.
View attachment 592259
Make sure you wear eye protection and gloves. I'm still carrying a steel splinter in my left wrist since 1970.
One other thing to check, make sure that the diff housing isn't slightly damaged from the side of the punch. I've seen that a few times.
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
Yeah that setup looks like it would work well. In hindsight, cutting the old ones off is pretty easy if you just jump right to that - if you wanted to skip buying one. But adding one of those to the kit would be nice.

This torquing the pinion nut is is the real beast part though - mainly because I'm on stands. If it was on a lift, I'd be done today. It is a crap ton of torque - 200-300ft lbs, on a freely rotating yoke. This is how the manual shows to do it, with the Mopar special tool - that guy must be WAY stronger than me. But again, much easier with lift clearances and working room - and I'm not especially strong to begin with.

1794704076977.png
 
OP
OP
C

chili81

Junior Member
Joined
Nov 3, 2026
Posts
15
Reaction score
23
Location
Connecticut
Ram Year
2014
Engine
5.7 Hemi
Yeah i bet that's what most private shops would do - just swap for a used axle. Remanufactured ones are like $3k. I assume dealer would just go new - idk how they operate.

Got it back together today except the cover and filling it back up (and putting brakes back on). Seems to have gone smoothly.
 

Grams

Senior Member
Joined
Oct 4, 2024
Posts
1,377
Reaction score
2,180
Location
Texas
Ram Year
2024 & 2015
Engine
6.7 Cummins & 5.7 Hemi
I was the rear axle tech for a Toyota dealership in the early ‘70s …and the way we determined shims for pinion-depth was to assemble and use dye on the ring gear to see the wear pattern on the two gears teeth.

But to have a shim beneath a cup is crazy…. and the actual Purpose of a crush-sleeve is to provide the proper bearing pre-load… so I wouldn’t be too worried about altering a sleeve as long as it was to shorten it.
 

Latest posts

Forum statistics

Threads
213,354
Posts
3,092,143
Members
174,575
Latest member
DITRIO
Back
Top